
1. Product & Industry Overview
Scenic areas, industrial parks and resorts buy sightseeing cars against the tourism peak, and the order rhythm of the electric sightseeing car assembly line follows the visitor calendar. The sightseeing car production line (also called a sightseeing bus or shuttle assembly line) completes final assembly of low-speed electric vehicles from chassis frame to road test; the class follows GB/T 21268 for non-road sightseeing vehicles, belongs to special-purpose in-plant motor vehicles, and requires use registration before service. The types: 6-11 seat electric sightseeing cars are the scenic-area backbone, open bodies with canopies; golf carts run 2/4/6 seats for courses and residential estates; vintage-styled cars serve featured routes; enclosed luxury versions add air conditioning. Quality control on an electric sightseeing car assembly line sits in three places — welded frame strength, battery pack fixing with harness protection, and brake-steering tuning; low speed is not low requirement, and full-load climbing plus driving range are hard acceptance figures.
2. Process Flow (see photo)
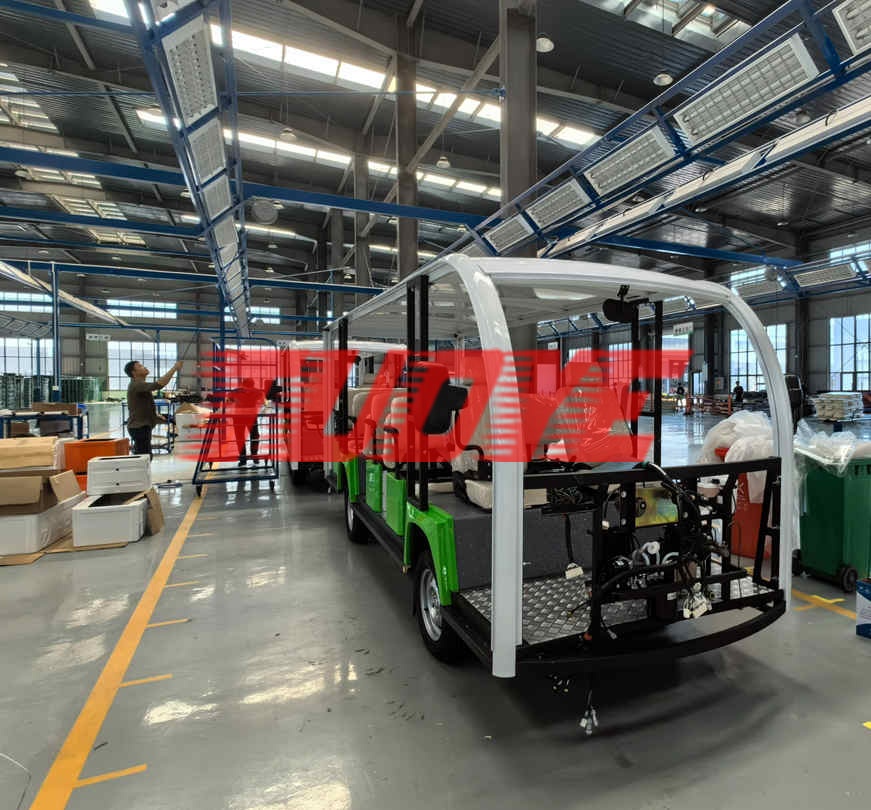
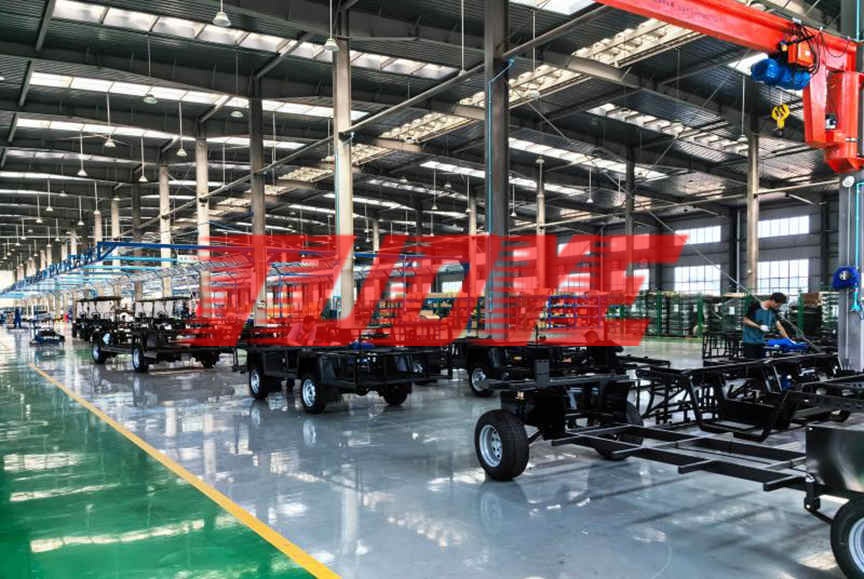
The photos show two sections of one sightseeing car production line. First: mid-to-late final assembly — sightseeing cars with white curved canopy frames and green side panels build at floor-marked fixed positions, beige multi-row seats just fitted still in protective film, front-end harnesses exposed awaiting dressing, black multi-tier tool trolleys at each station, 2-3 build points flowing lengthwise. Second: the chassis marriage section — square-tube frames in a single file of 10-15 down the shop depth, axles, wheels and steering installed, upper structures waiting; on the right a red KBK rail carries blue chain hoists moving batteries and frame parts, the green main lane zoned in yellow markings, roof daylight bands lighting the hall. Assembly sequence: chassis frame on line → rear axle, motor and drive → steering front axle → brake lines → battery pack hoisted and wired → controller and instrument harness → roof pillars and canopy → body panels → seats and flooring → lamps and mirrors → whole-vehicle road test with water-test sampling.
3. Customization & Service
Customization: station layouts compatible across the seat-count range, KBK hoist points checked against battery and frame weights, road-test stations fitted with ramps and grounds per GB/T 21268. Tuoye — in Wenling, Taizhou, Zhejiang, China — delivers the electric sightseeing car assembly line from in-plant pre-assembly and commissions through trial production, warranty one year, tool trolleys and KBK parts supplied long-term; pre-season station expansions and added buffers are taken on short notice. For a quotation and lead time, send the seat-count range and annual capacity — fixed-position versus slow-flow layouts compared for your program.
Paint-to-final-assembly handoff must run smooth: shell parts delivered in vehicle order, soft buffer racks at the panel stations of the electric sightseeing car assembly line — dent-and-respray is the schedule killer of the peak season. At the upper-structure stations, pillar and canopy marriage get auxiliary locating fixtures; wherever crews share a station, the locating points carry the quality, not hand feel. The off-line section of the sightseeing car production line zones queuing by delivery batch — charging, preparation and inspection in one flow; and if enclosed-cabin models come onto the sightseeing car assembly line, the air-conditioning and sealing stations enter the layout at design time, because retrofitting stations later moves the main line, at no small cost.