Inverted-Assembly Fixtures and Off-Line Verification on a Bicycle Assembly Line
1. Industry Overview
Bicycle manufacturing runs domestic volume and shared-bike mega-tenders in parallel — shared tenders drop hundreds of thousands of units, and poka-yoke and verification configure for bulk delivery. A bicycle assembly line — the trade also says bicycle production line — completes final assembly from frame on-line to whole-bike verified off-line. Safety follows the GB/T 3565 series, braking performance and frame/fork strength as mandatory figures; types split shared bikes, commuters, mountain bikes and city leisure bikes. Shared models are designed maintenance-free — solid tires and shaft drive cutting after-sales — and operators' durability and consistency demands translate into verification intensity, braking and drivetrain data becoming acceptance evidence.
2. Process Flow & Line Configuration
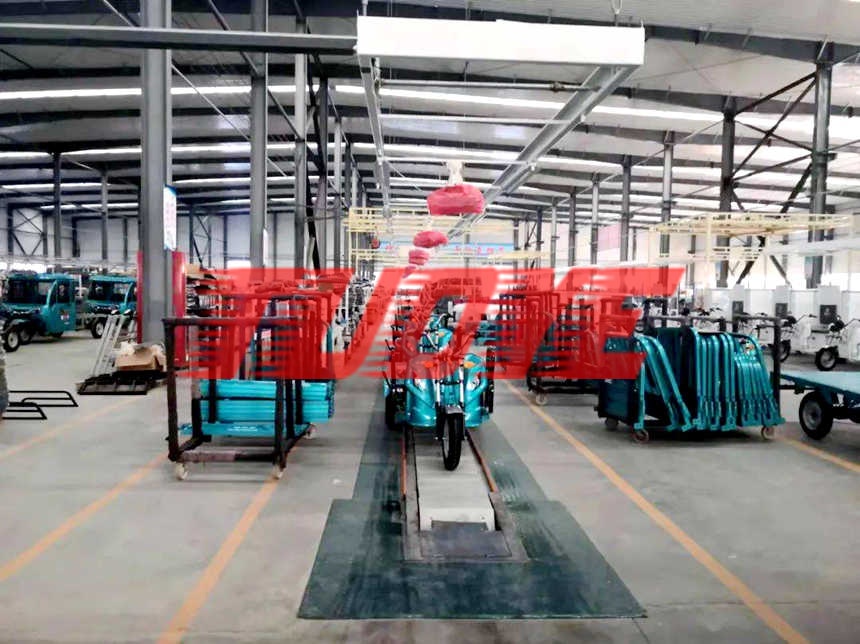
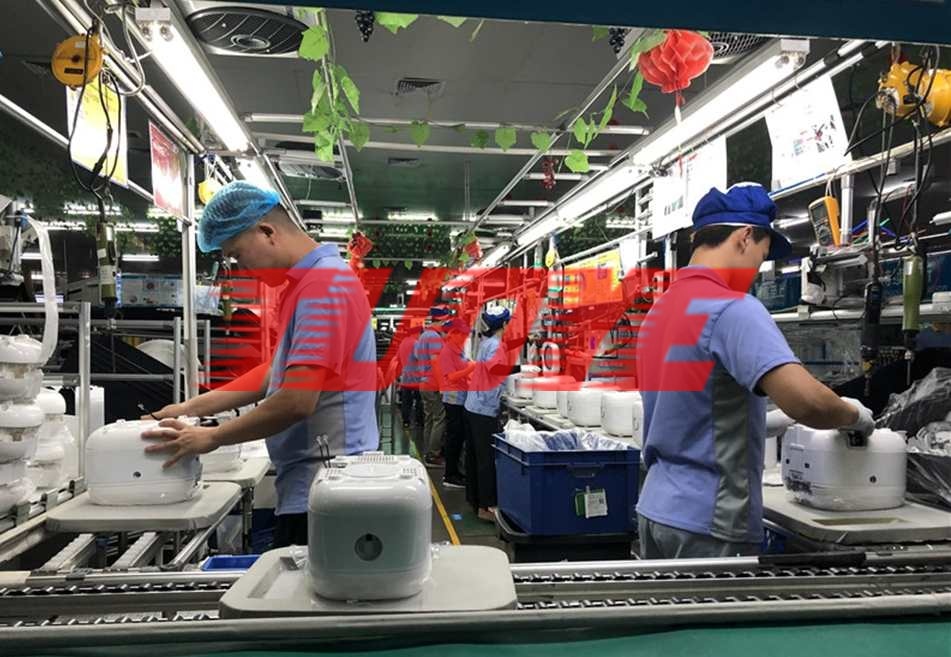
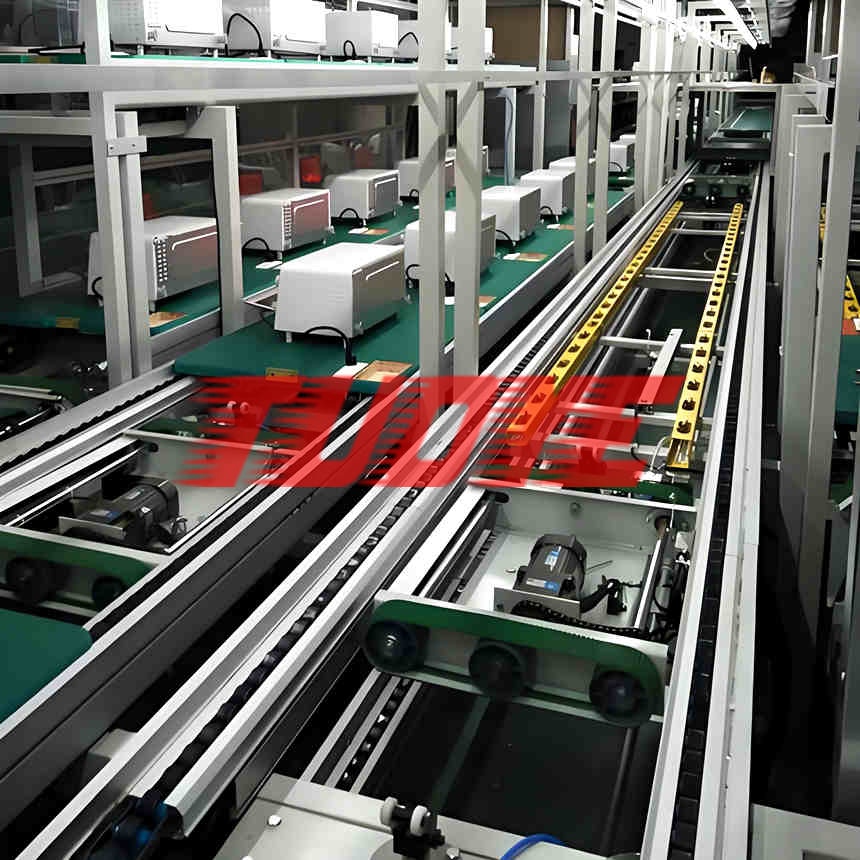
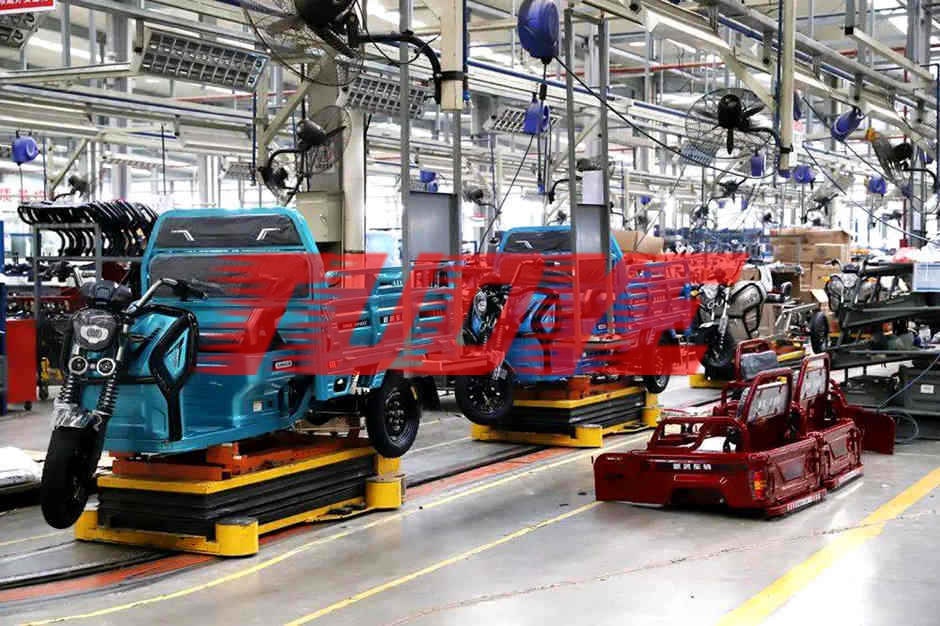
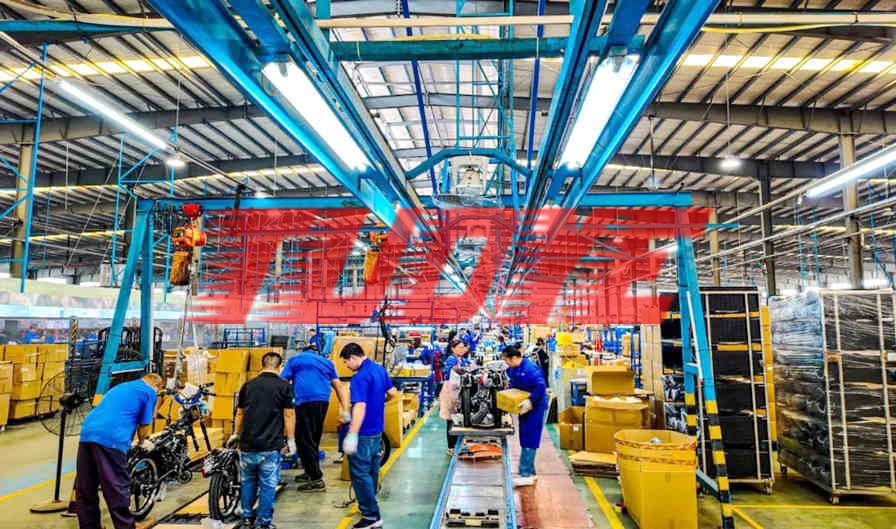
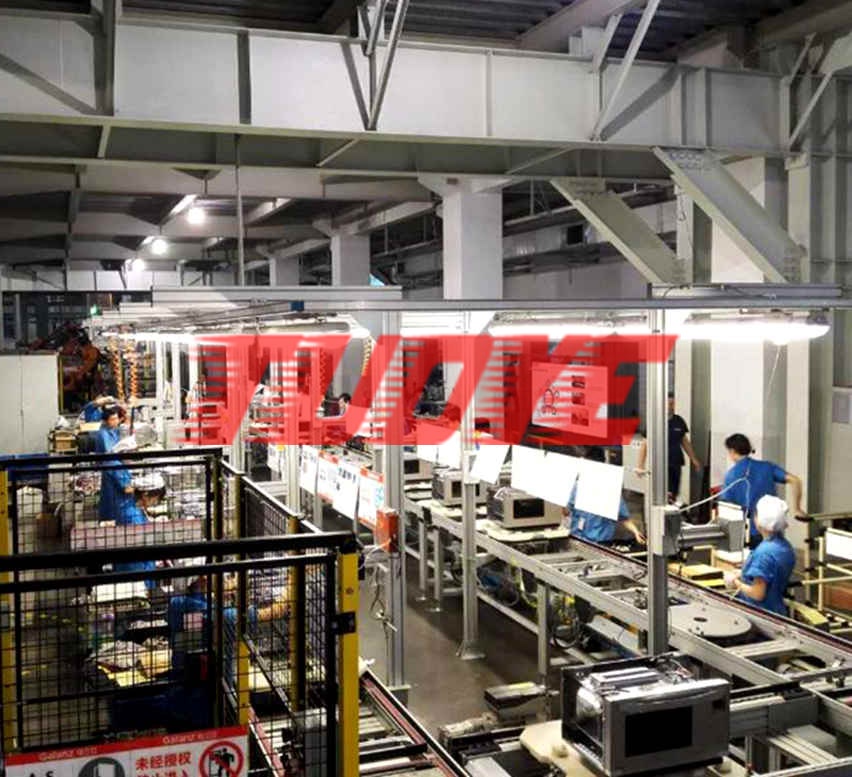
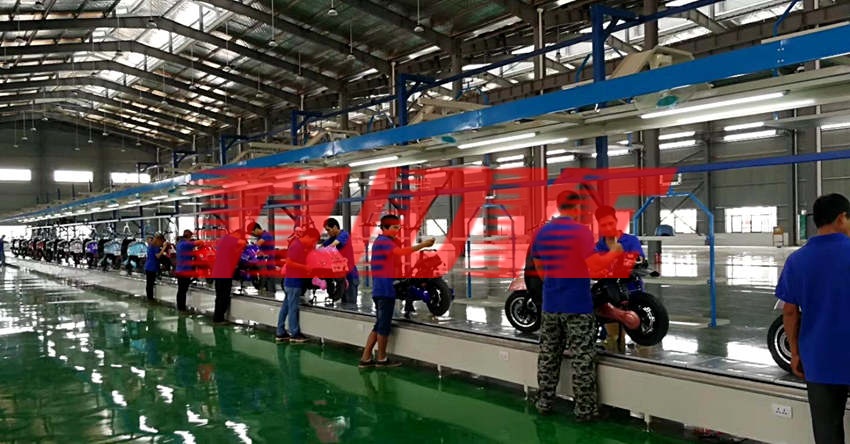
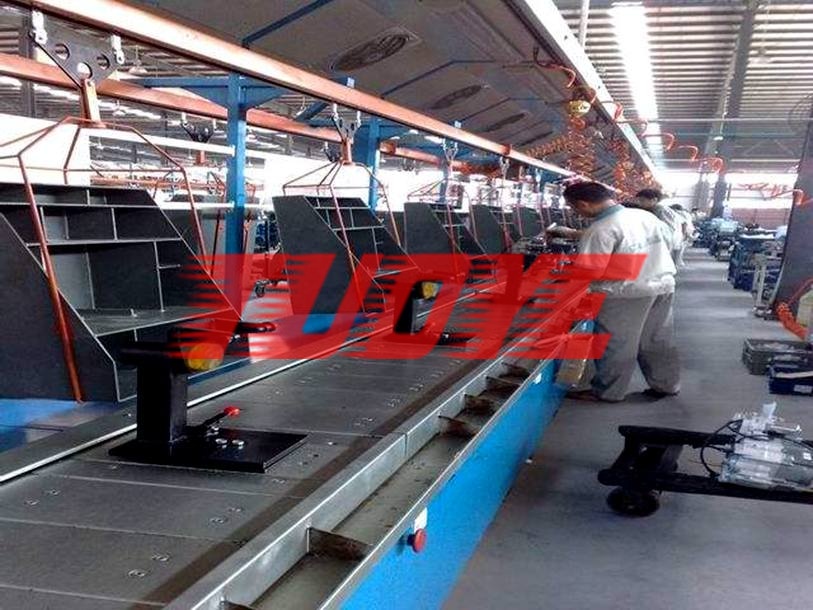
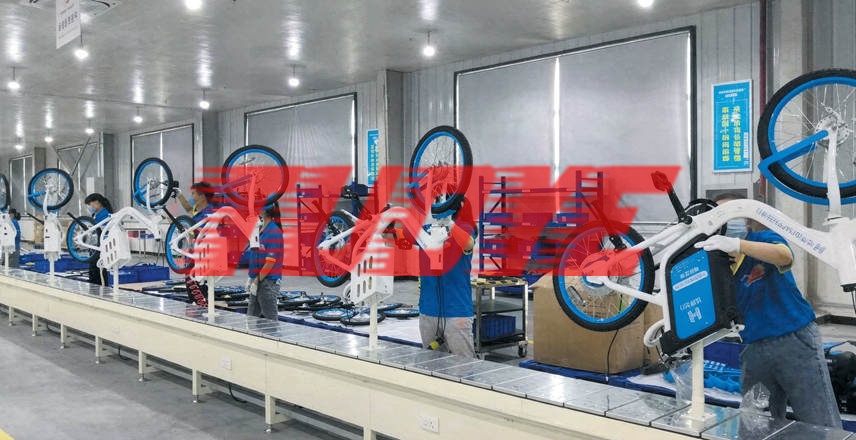
The typical bicycle flow: frame on line (inverted, located) → headset and bottom bracket press-fit → fork assembly → wheel sets → drivetrain (chainwheel, chain, freewheel) → handlebar and seat post → brake assembly and adjustment → derailleur tuning → bike righted → off-line verification → packing or caged dispatch. In a delivered project, the bicycle production line runs bench-style conveying with flip fixtures locating on the bottom bracket and head tube — the inverted attitude easing bracket and drivetrain work — 12-15 stations at one-to-two minutes a bike.
3. Configuration & Selection Tips
Fixture V-blocks adjust to head-tube angle, so shared-to-sport model changes never re-cut tooling; press stations carry vertical presses with force monitoring, headset and bracket precision feeding handling directly. Off-line verification records braking force, wheel trueness and chain tension — shared operators' acceptance sampling runs on those records; smart-lock stations add network unlock testing, scan-verified unit by unit. The bicycle assembly line organizes as main plus sub-assembly — wheels and handlebars built on branches and merged; lacing and truing run machine-done on the branch, runout eliminated before the main line. Painted frames travel in padded multi-tier racks, scratch defects managed at the transfer link.
4. Delivery & Service
From model range and daily capacity, Tuoye — in Wenling, Taizhou, Zhejiang, China — issues the bicycle assembly line proposal with verification aligned to the order's acceptance standard; equipment enters after in-plant pre-assembly and commissions through trial production. One-year machine warranty, flip fixtures, plate chain and air-tool parts supplied long-term, plus temporary expansions before shared-bike tender deliveries.
Permanent link: https://www.liushuixian.com/post/inverted-assembly-fixtures-and-off-line-verification-on-a-bicycle-assembly-line.html
Disclaimer: Some articles on this site are compiled from public technical sources for reference. If any content infringes your rights, please contact us for removal. Please credit the source when reprinting.