The Mechanical Characteristic Test Section on a Vacuum Circuit Breaker Assembly Line: VS1 Assembly Essentials
1. Industry Overview
Center-mounted 12 kV cabinets keep VS1-class vacuum breakers in volume growth, and both switchgear makers and breaker specialists hold their expansion pace — assembly-test capacity now decides delivery cycles. A vacuum circuit breaker assembly line — the trade also says VCB production line — completes final assembly of VS1/VD4-class indoor breakers from mechanism frame on-line through whole-unit characteristic testing. Products follow GB/T 11022 and GB 1984; poles split solid-embedded and assembled types, drawout structures serve center cabinets, and rated currents 630-3150 A match the cabinet range.
2. Process Flow & Line Configuration
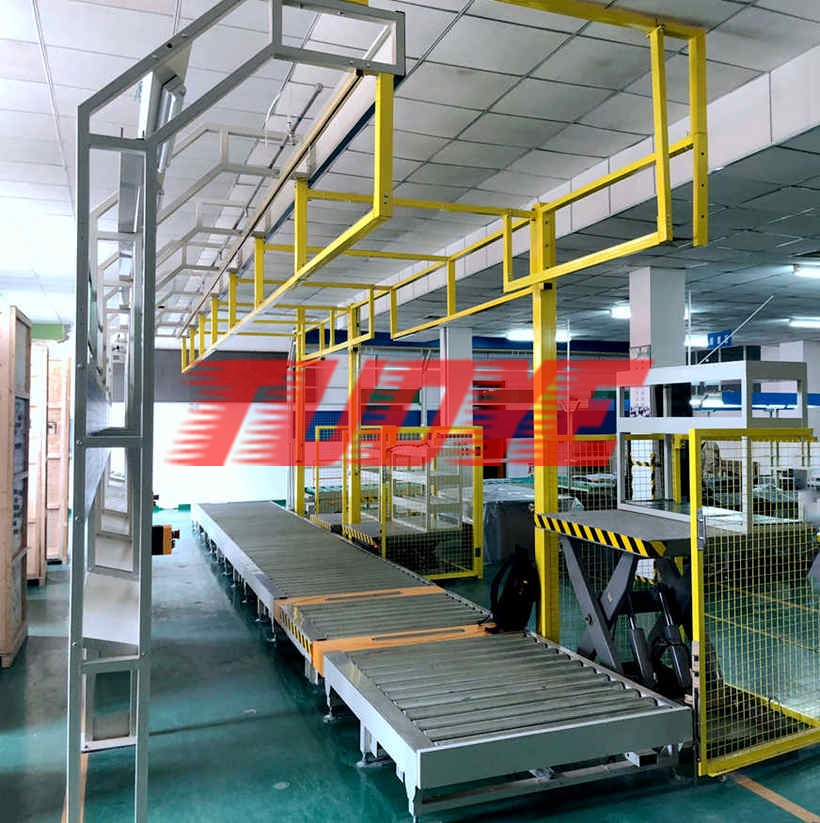
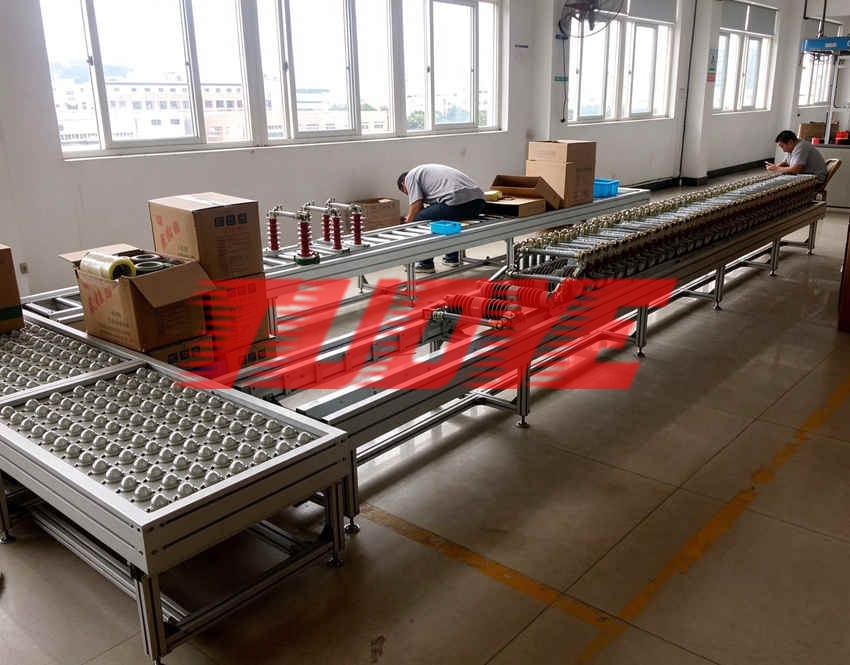
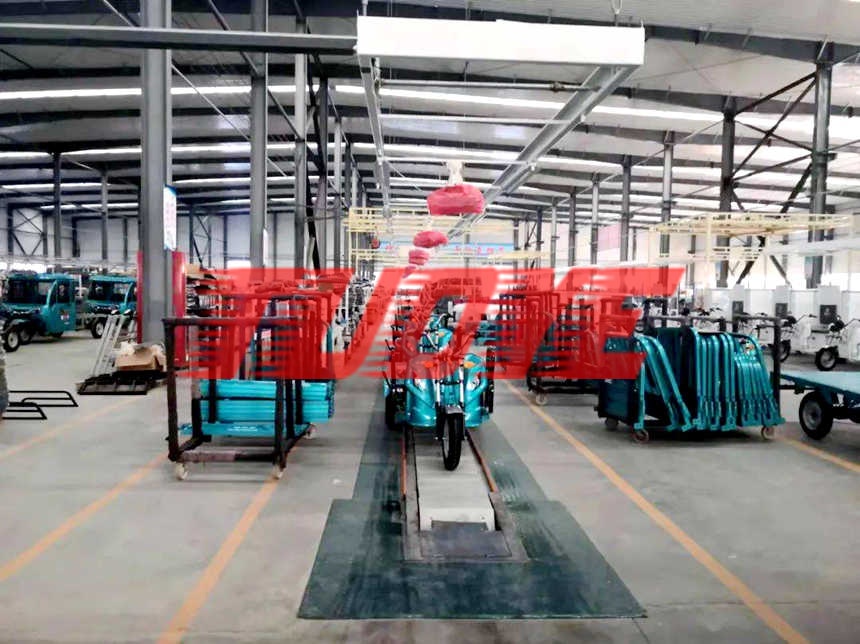
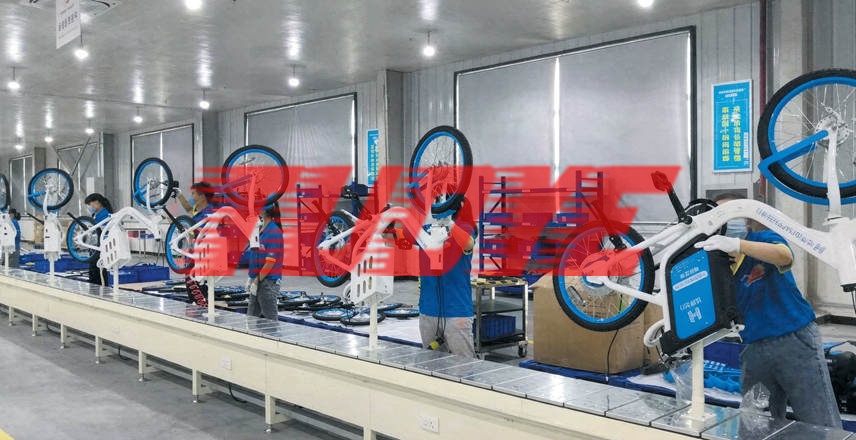
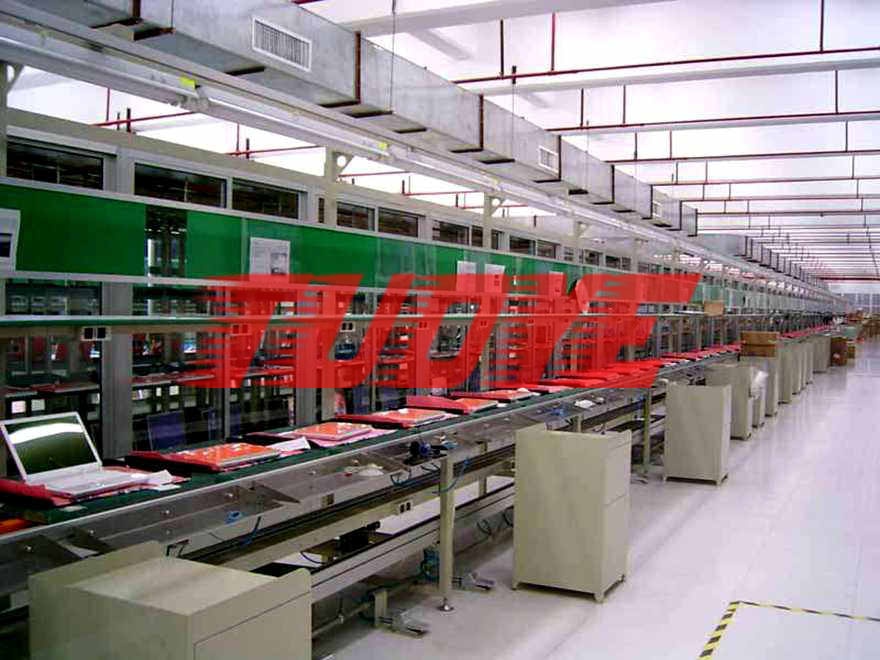
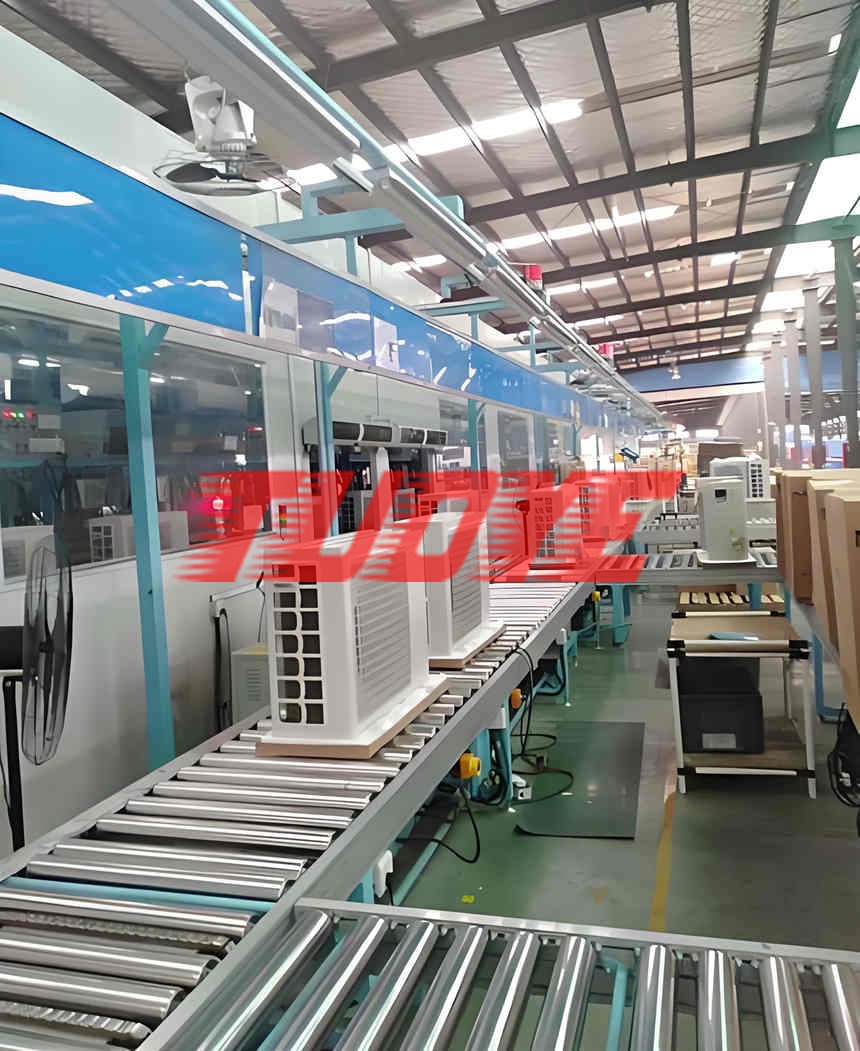
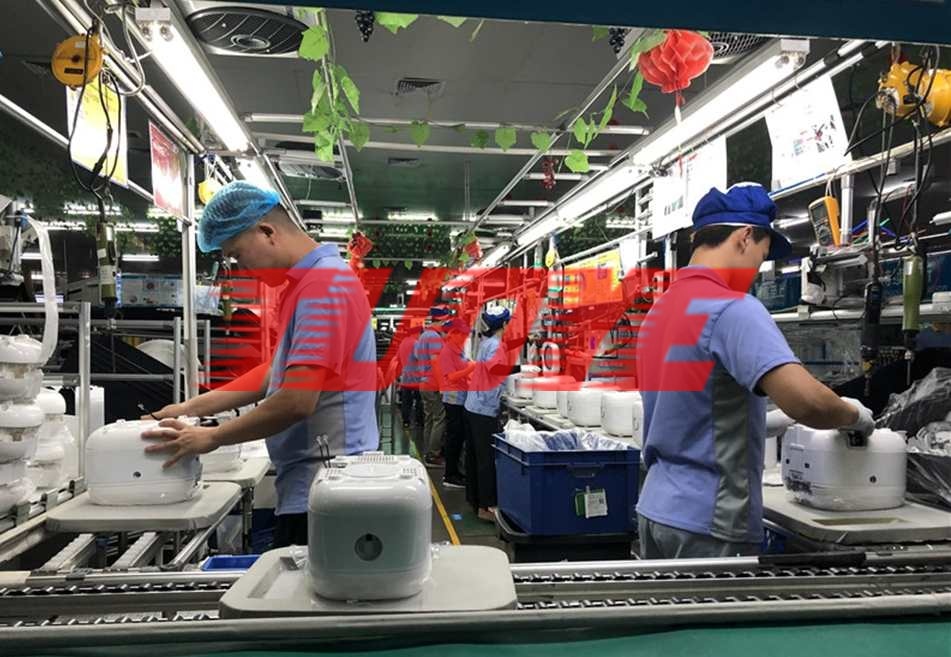
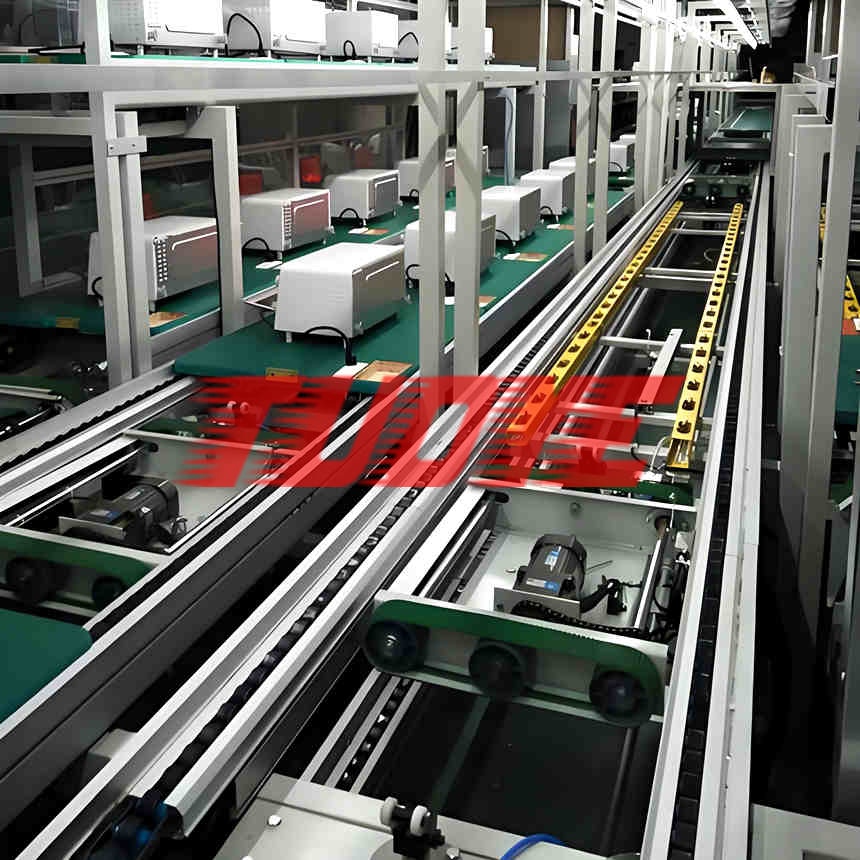
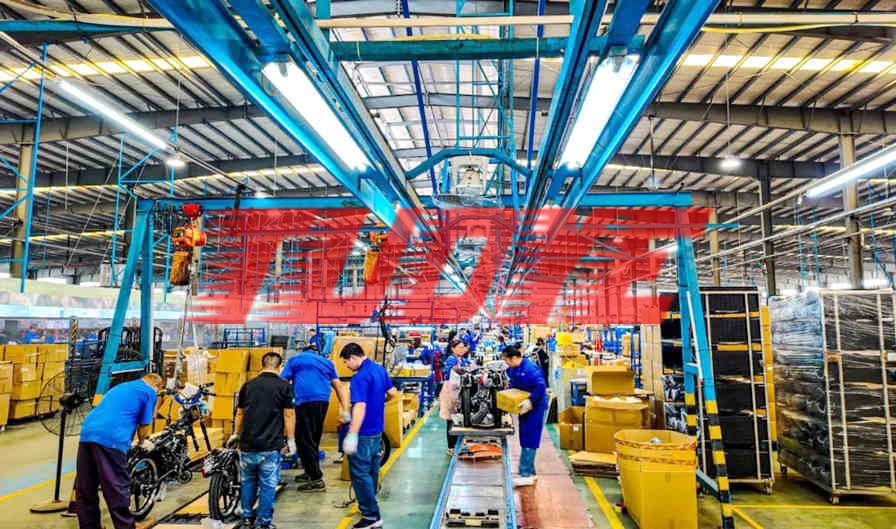
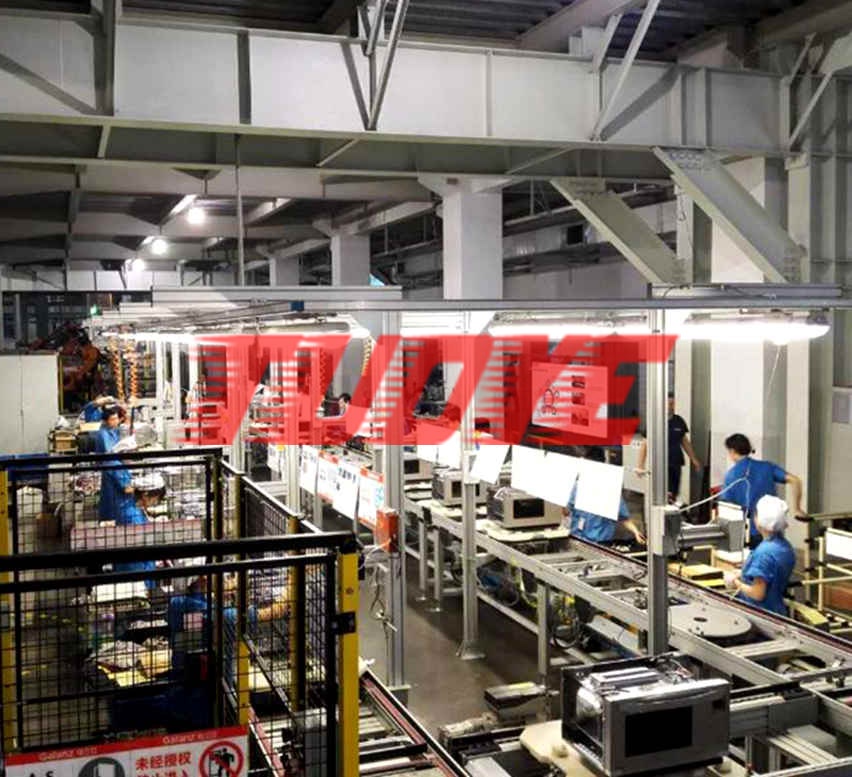
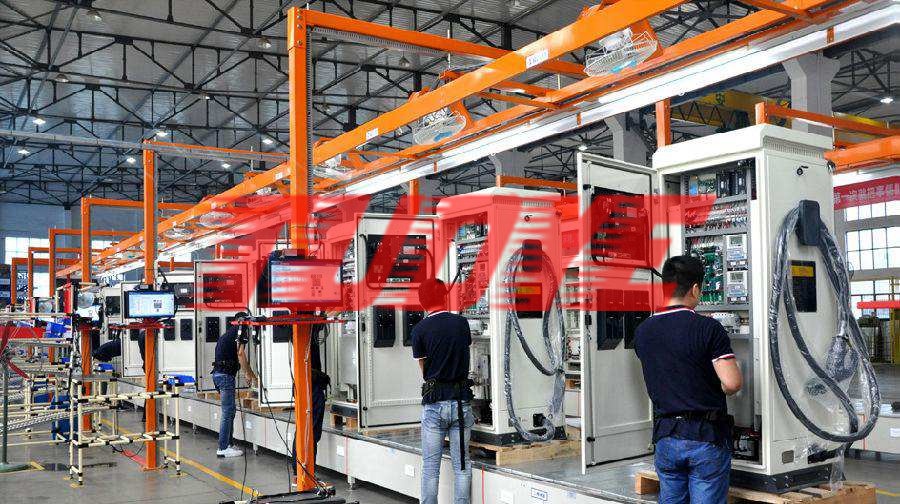
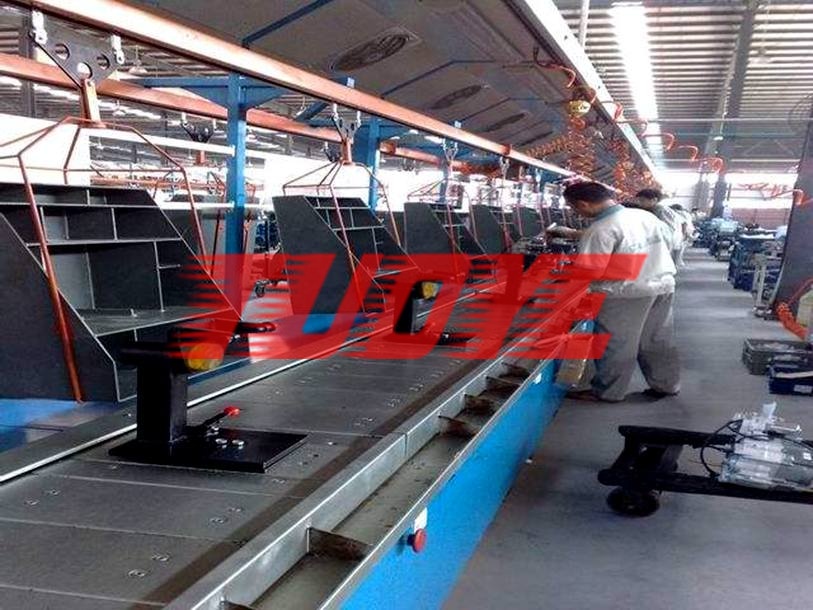
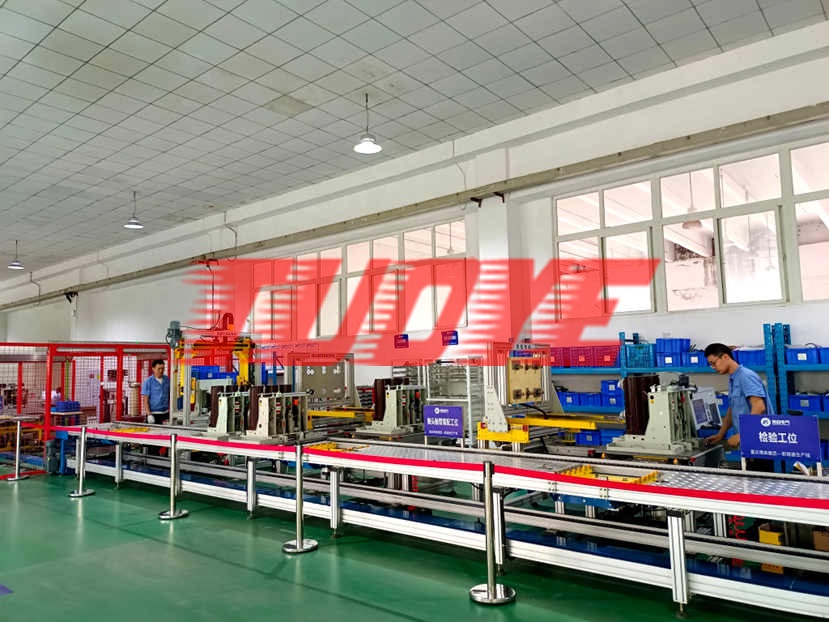
The typical VS1 flow: mechanism frame on line → pole columns and vacuum interrupters assembled → primary circuit connection (contact seats and tulip contacts) → insulation pull-rods and drive links → spring operating mechanism (charging motor, open/close coils) → secondary plugs and auxiliary switches → mechanical characteristic test → main-circuit resistance and power-frequency withstand → chassis truck assembly and insertion commissioning → nameplate and packing. In a delivered project, the breaker assembly line runs a wide speedchain, pallets with locating pins carrying bodies station to station, a servo press handling contact-seat and pin press-fits, flip fixtures enabling two-side work, 10-14 stations with the test zone isolated per HV safety rules.
3. Configuration & Selection Tips
Characteristic test benches record open/close times, three-phase synchronism, travel and overtravel — bounce and synchronism out of tolerance adjust and retest at the same station; tulip-contact finger springs get gauge-checked group by group, uneven pressure closing into local heating. Interrupters travel from unboxing to assembly inside clean stations — dust control on ceramic shells is insulation reliability; the withstand zone takes isolation interlocks and grounding with automatic rise/fall curves. The truck section fits insertion rails per chassis model, engagement with contact boxes verified on-line. Pallets serialize to frame and pole-center distances, and test data archives by serial number for the switchgear makers' audits.
4. Delivery & Service
From specification range and monthly capacity, Tuoye — in Wenling, Taizhou, Zhejiang, China — issues the VCB production line proposal with test-section instruments on the equipment list; equipment enters after in-plant pre-assembly and commissions through trial production, acceptance covering first-pass characteristic rate and beat compliance. One-year machine warranty, pallets, speedchain and test-bench parts supplied long-term, plus automatic-testing and traceability retrofits on existing lines.
Disclaimer: Some articles on this site are compiled from public technical sources for reference. If any content infringes your rights, please contact us for removal. Please credit the source when reprinting.