Charging and Pull-Down Test Section Configuration on a Refrigerator Assembly Line
1. Industry Overview
The household refrigerator market runs big-capacity and inverter models, with side-by-side and multi-door shares climbing yearly — lines adjust toward big-cabinet loading and expanded testing. A refrigerator assembly line — the trade also says refrigerator final assembly line — completes final assembly from cabinet on-line to whole-unit packing. Products follow GB/T 8059 with efficiency filed per GB 12021.2; structures run two-door, three-door, side-by-side and French multi-door, frost-free models adding air-duct and defrost stations over direct-cool types. As inverter compressors and dual-circuit systems spread, electronics assembly gains weight, and plants commonly move the electronics pre-check stations upstream to cut late-stage electrical rework.
2. Process Flow & Line Configuration
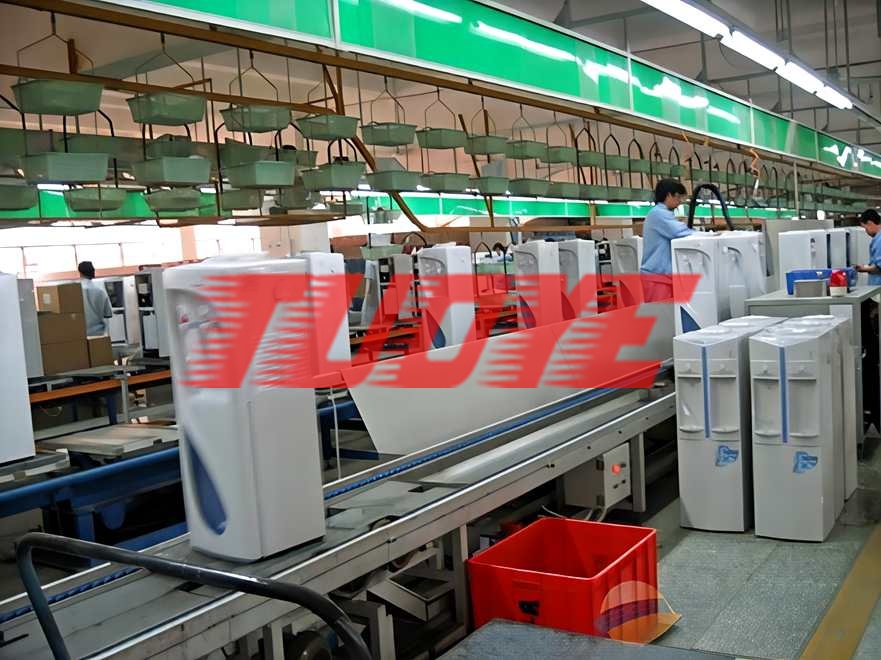
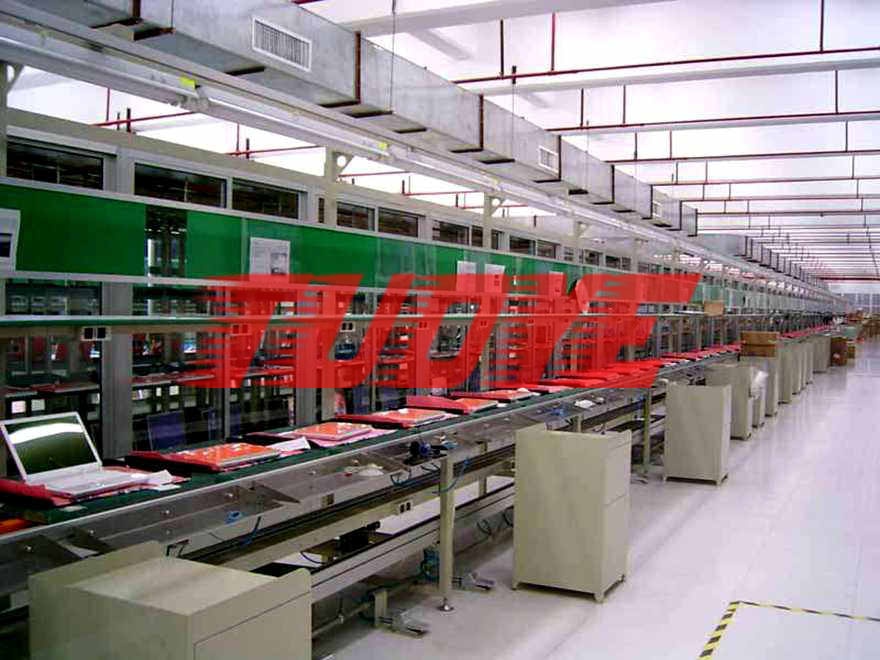
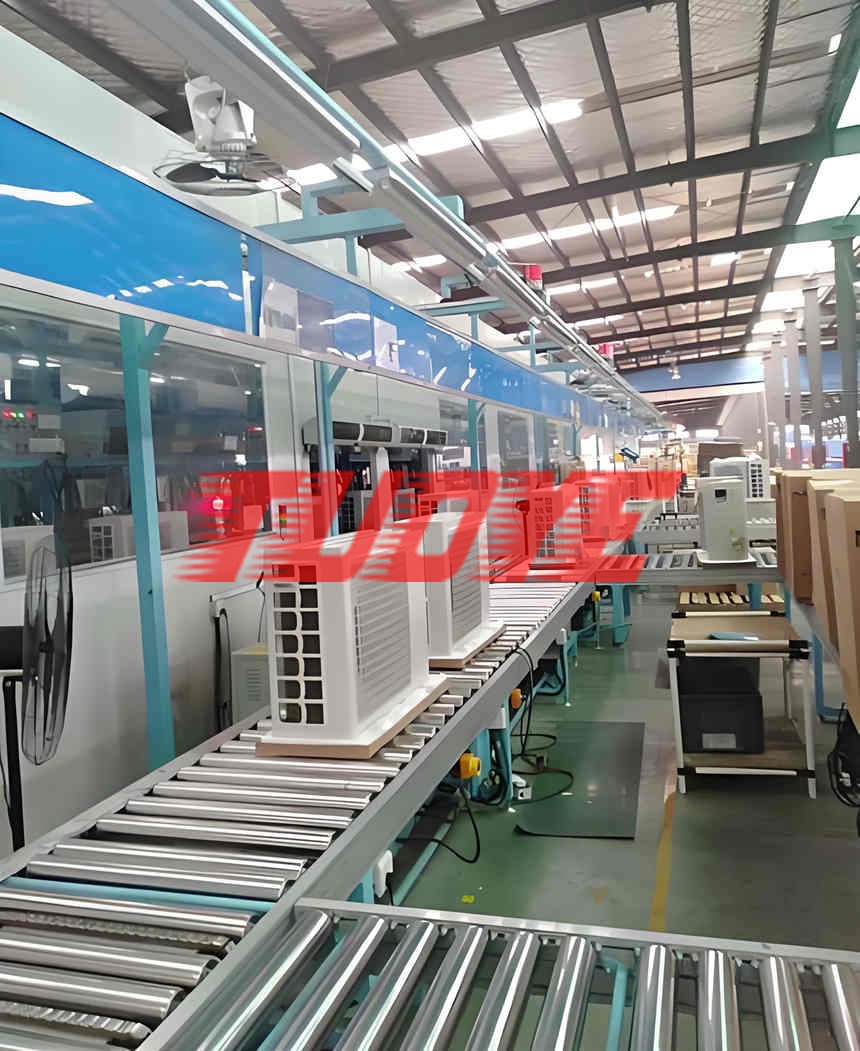
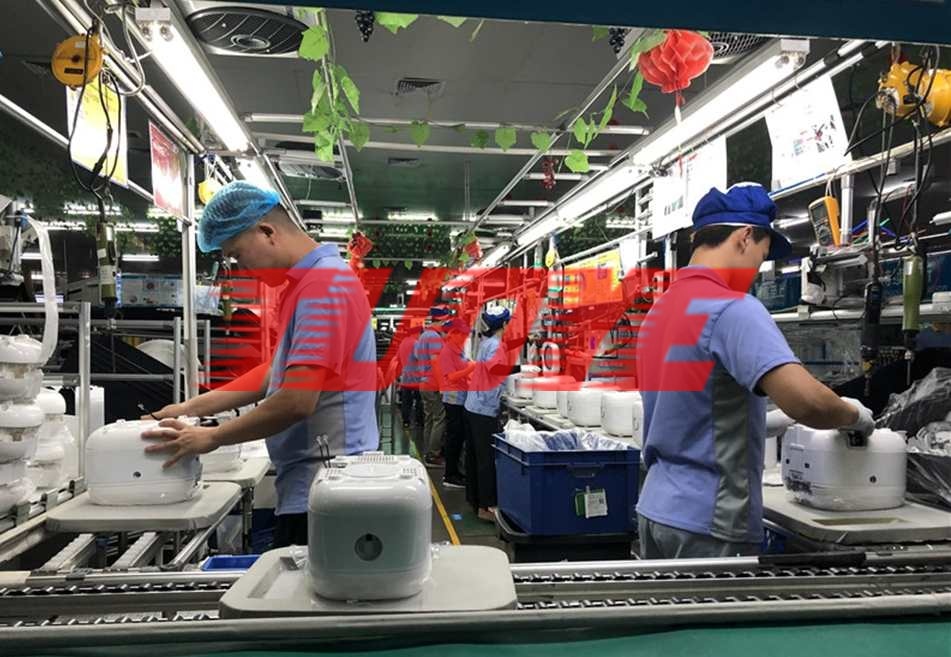
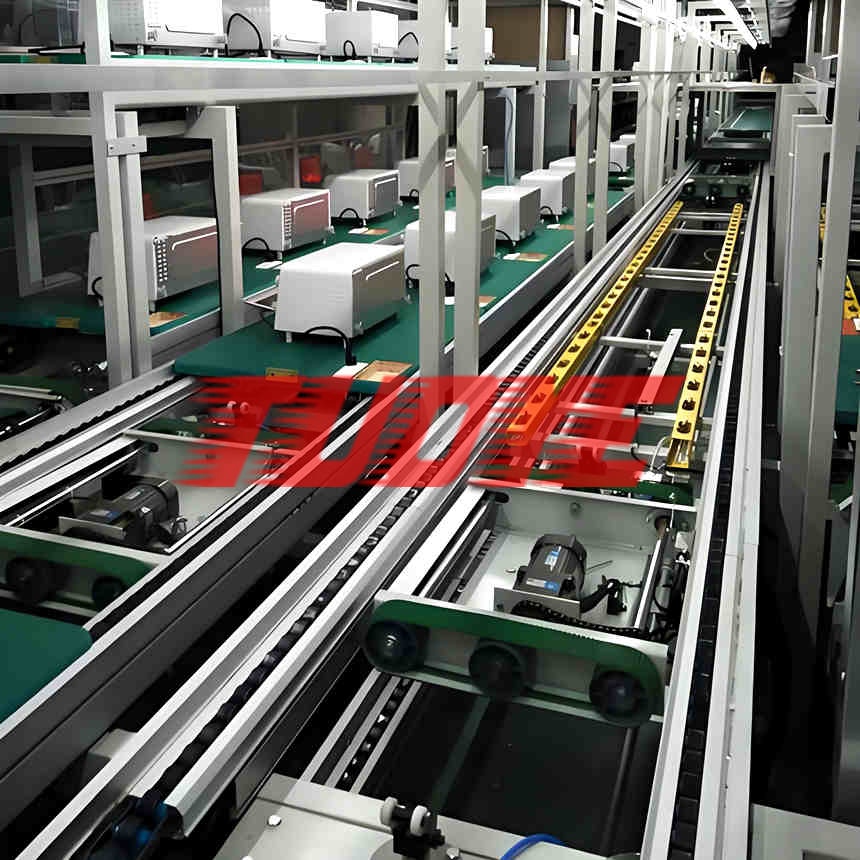
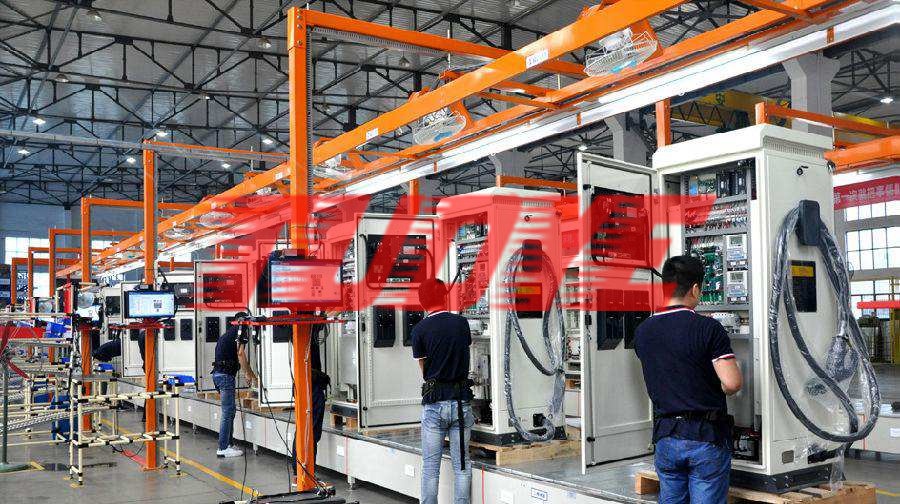
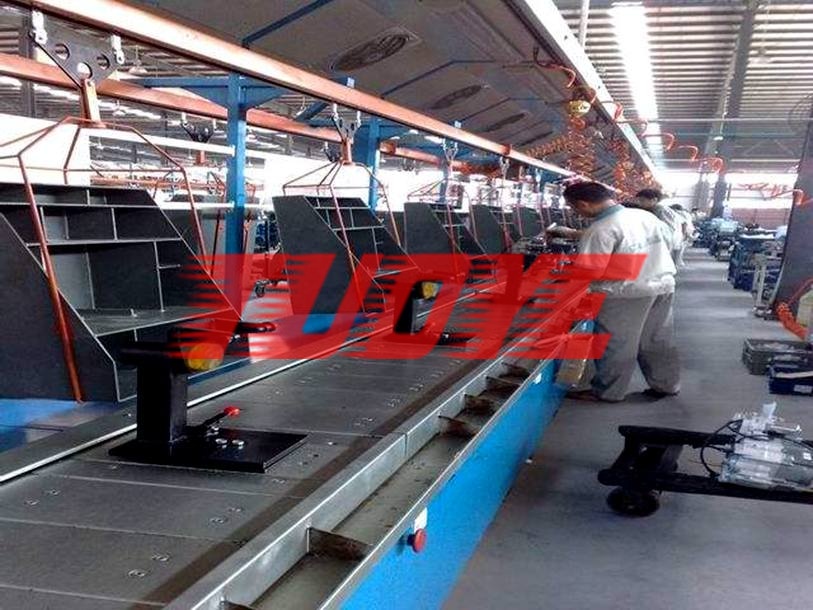
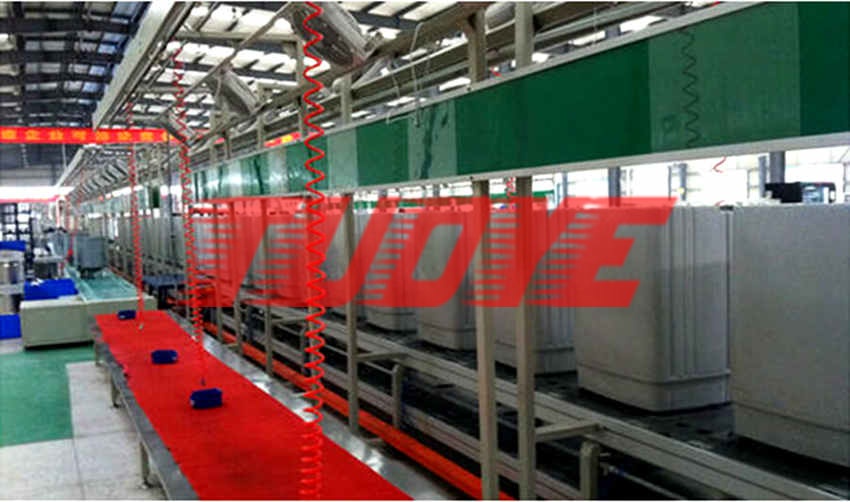
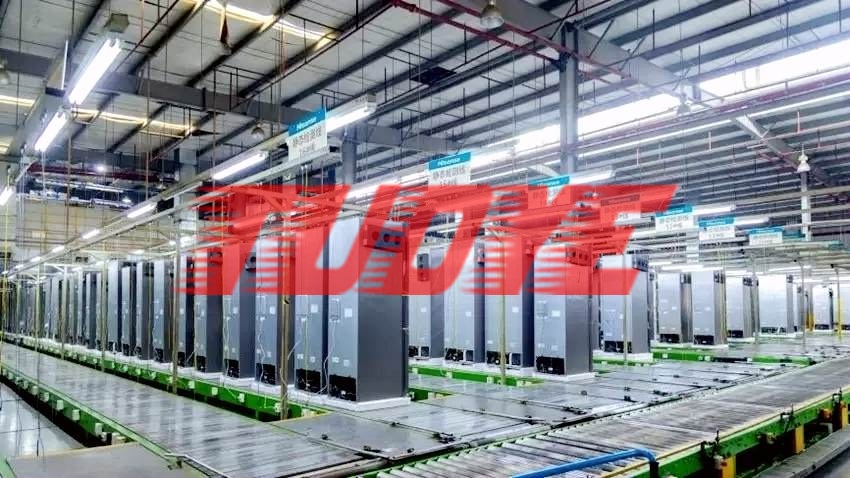
The typical refrigerator flow: cabinet on line (foamed body incoming) → compressor bay assembly → pipe welding → nitrogen hold & leak check → vacuum → metered charging → thermostat and lighting electricals → door assembly → powered pull-down test → appearance final check → labeling and packing. In a delivered project, the refrigerator production line runs a two-tier plate chain — pallets carrying big cabinets above, empties returning below — 25-30 stations per side at a 30-60 second beat, with side-by-side pallets serialized to cabinet-base locating holes.
3. Configuration & Selection Tips
The test section is the beat-critical point of a fridge assembly line: pull-down duration is rated per model, test-room slots counted backwards from daily program and test duration, and expansions add test rooms first. The charging section carries explosion-proofing for R600a, charge weights metered on electronic scales and recorded unit by unit; the door-gasket station uses dedicated locating tooling, since magnetic-gasket flatness feeds the energy figure directly. Curve radii on the refrigerator production line size up for the tallest cabinets with guards raised to match — transfer knocks cost more than tooling. Doors join from a sub-assembly line, hinge and gasket precision verified before merging; pull-down temperature recorders channel per model, data archived with efficiency sampling results.
4. Delivery & Service
From cabinet size band, daily program and workshop length, Tuoye — in Wenling, Taizhou, Zhejiang, China — issues the refrigerator assembly line proposal, comparing dual parallel and single loop at layout stage; equipment enters after in-plant pre-assembly and commissions through trial production. One-year machine warranty, pallets, plate chain and charger parts supplied long-term, plus station densification and test-room expansion on existing lines.
Permanent link: https://www.liushuixian.com/post/charging-and-pull-down-test-section-configuration-on-a-refrigerator-assembly-line.html
Disclaimer: Some articles on this site are compiled from public technical sources for reference. If any content infringes your rights, please contact us for removal. Please credit the source when reprinting.