The Characteristic Test Section of a Pole-Mounted Switch Assembly Line: Mechanical Characteristics, Withstand Voltage and Circuit Resistance
1. Industry Overview
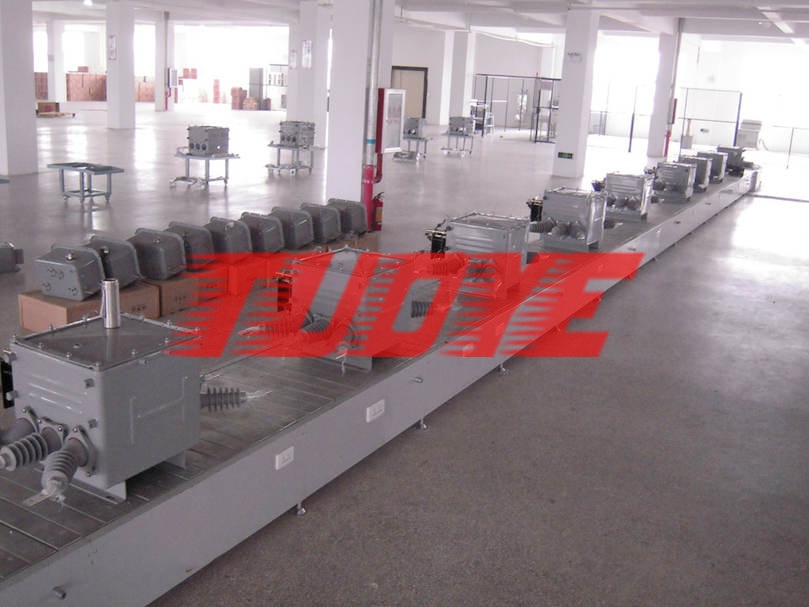
As distribution automation reaches county and township lines, annual pole-mounted vacuum breaker purchases keep growing, and makers expand capacity from final assembly and testing first. A pole-mounted switch assembly line — the trade also says pole-mounted breaker assembly line — completes final assembly from tank on-line through characteristic testing. Products follow GB/T 11022 and GB 1984; structurally, ZW20 box-type and ZW32 cylindrical series dominate, with pole-mounted load switches and integrated primary-secondary sets sharing the same lines. Distribution procurement runs on provincial centralized tenders with delivery windows bound to outage plans — so test capability and delivery rhythm must be planned into the line from the build stage.
2. Process Flow & Line Configuration
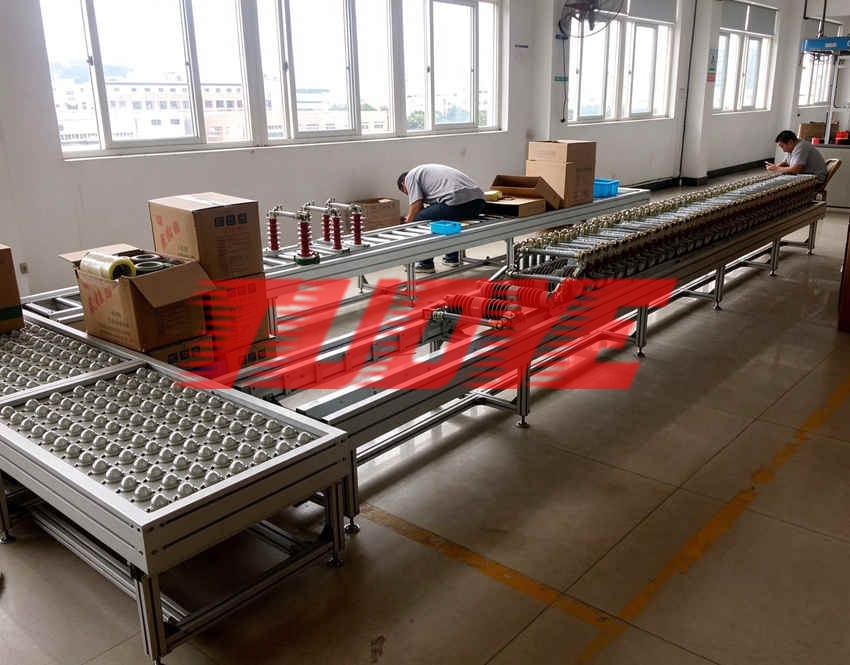
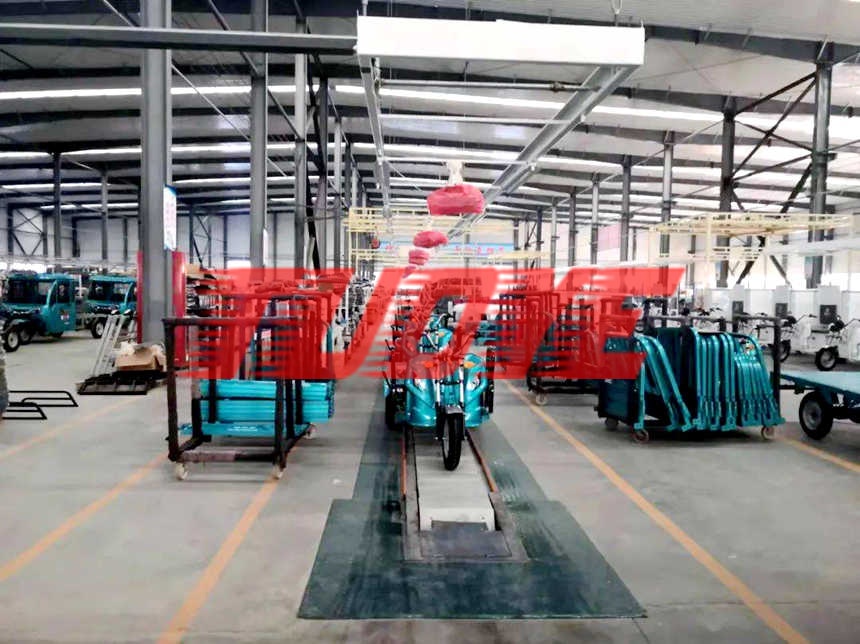
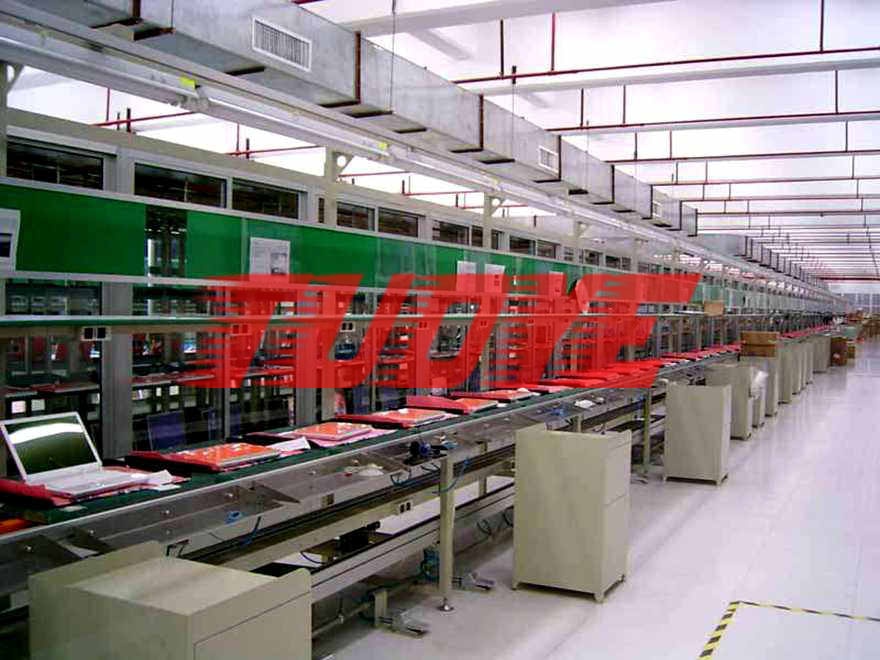
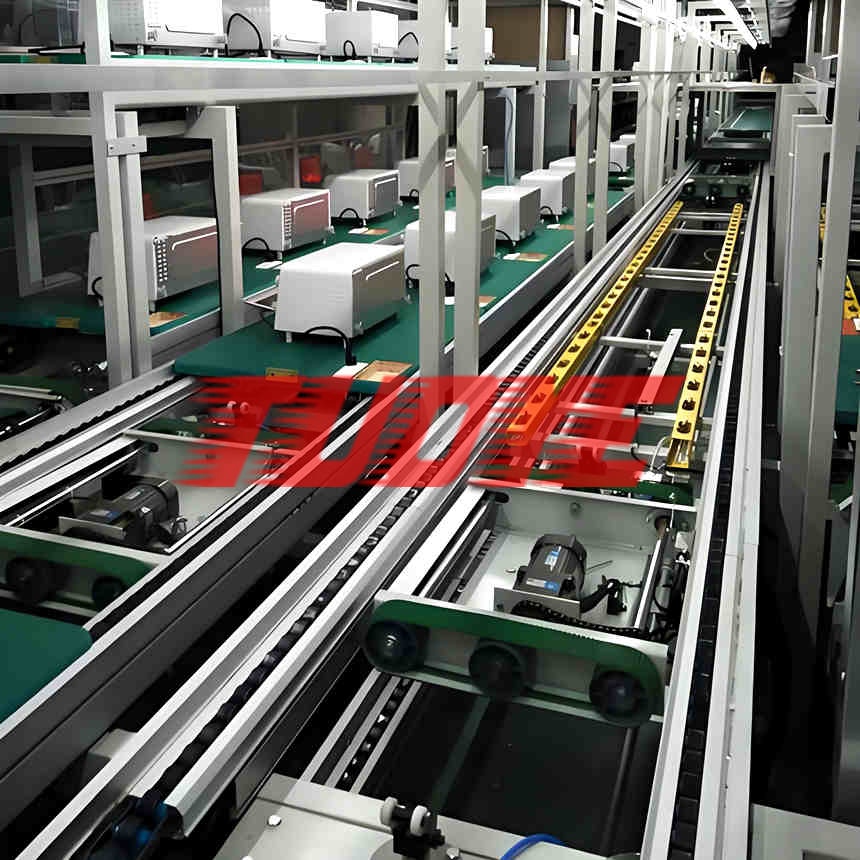
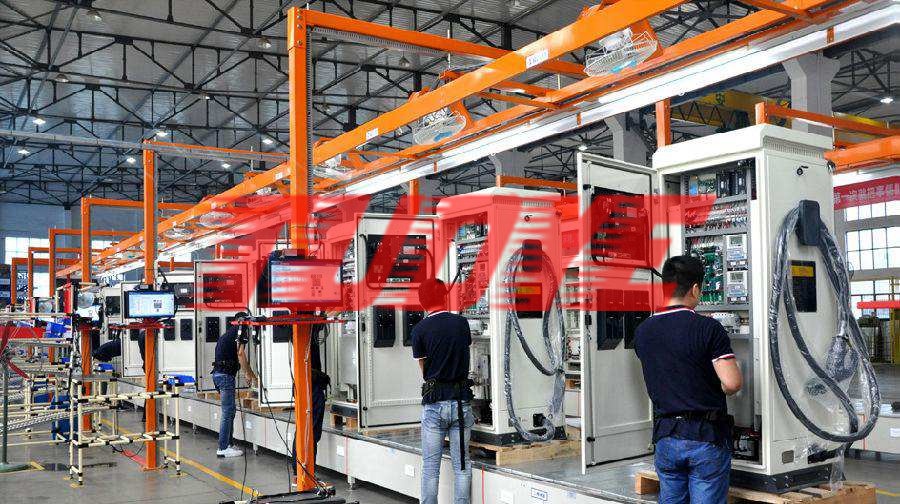
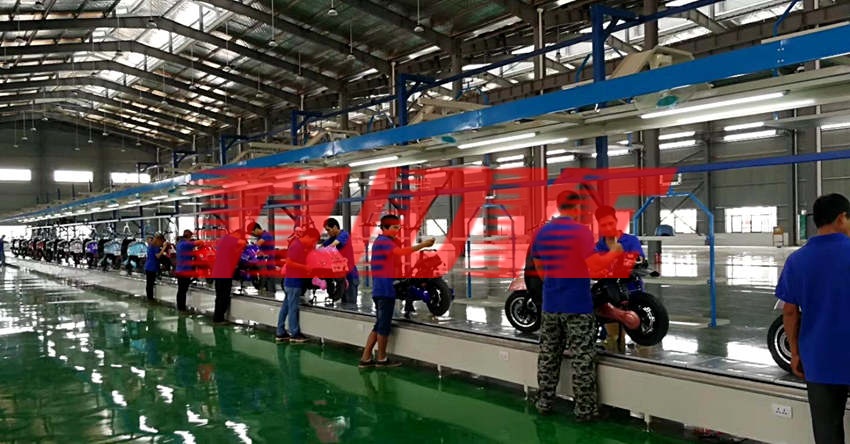
The typical pole-mounted vacuum breaker flow: tank on line → partition plates and flexible links → vacuum interrupter installed → main circuit connection → spring or permanent-magnet mechanism → outgoing bushings and support insulators → secondary control unit and aviation sockets → mechanical characteristic test → power-frequency withstand and circuit-resistance test → hardware and packing. In a delivered project, the pole-mounted switch production line runs a bench-style conveying line, steel deck in yellow-black edging, 12-15 stations single-side; testing splits into three points — characteristics, withstand, circuit resistance — so upstream deviations rework at the station where they're found.
3. Configuration & Selection Tips
The vacuum interrupter station takes a clean working zone — skirted insulators and interrupters are both dust-sensitive; main-circuit fastening uses torque tools, contact resistance tested and recorded unit by unit. Integrated primary-secondary models reserve FTU commissioning and powered burn-in positions, telemetry verified item by item; the withstand zone takes code-mandated isolation and grounding interlocks. Tooling on the pole switch assembly line serializes across ZW20, ZW32 and load-switch tank sizes, model swaps changing only the locating set. Characteristic test benches record open/close times, three-phase synchronism and travel curves, data archived by batch; bushings and insulators travel in dust-proof packaging, with pre-assembly cleanliness checks written into the process files.
4. Delivery & Service
From model range and monthly capacity, Tuoye — in Wenling, Taizhou, Zhejiang, China — issues the pole-mounted switch assembly line proposal; equipment enters after in-plant pre-assembly and commissions through trial production, with schedules run backwards around type-test sampling. One-year machine warranty, benches, tooling and test-bench parts supplied long-term, plus characteristic-test and FTU-section retrofits on existing lines.
Disclaimer: Some articles on this site are compiled from public technical sources for reference. If any content infringes your rights, please contact us for removal. Please credit the source when reprinting.